Need Help: All Types of Mechanical Seals & Spares, Call 0120-4923910
Chemical Processing Sealing Solutions
OEM Engineered Industry Solutions
Chemical Processing Mechanical Seals & Sealing Systems
Engineering Focus: Engineered Corrosion-Proof Sealing for Acids, Alkalis, and Hostile Process Solvents
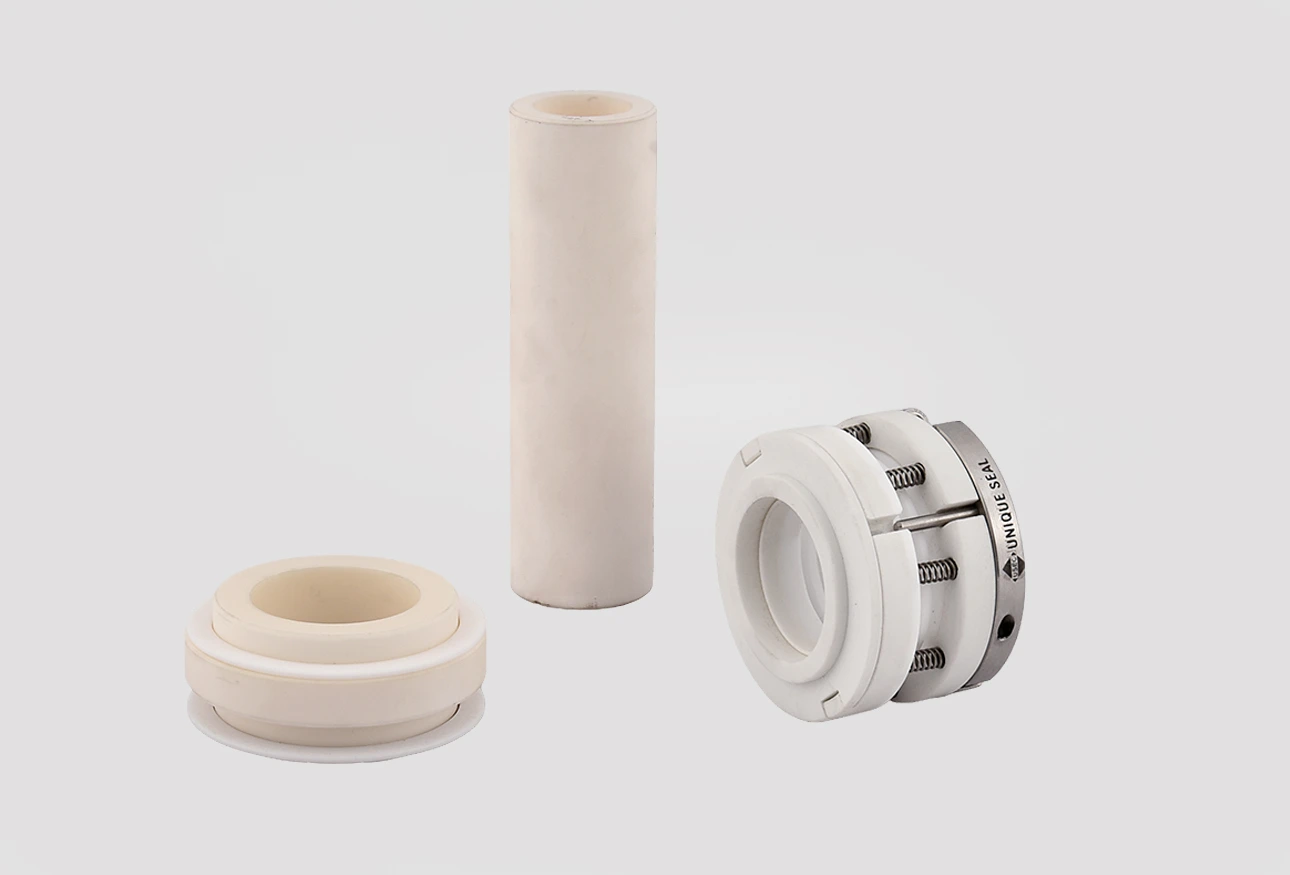
Chemical manufacturing and processing environments subject mechanical seals to aggressive chemical attack, thermal shock, and hazardous vapor emissions. From concentrated sulfuric, nitric, and hydrochloric acids to chlorinated solvents and aromatic hydrocarbons, seal failures risk plant safety and environmental fines. USEC delivers non-metallic PTFE bellows seals and specialized metallurgy for zero fugitive emissions.
The chemical industry deals with highly corrosive and hazardous materials; therefore, robust sealing solutions are required. Seals engineered to withstand aggressive chemicals, extreme temperatures, and challenging pressure conditions ensure safe and efficient operation for our clients.
Be it reactors or transfer pumps, we have solutions that enhance the performance and reliability of critical equipment so that they live up to the demanding standards of the chemical industry.
Critical Operating Challenges in Chemical Processing
Severe Acid Corrosion
Strong oxidizing acids rapidly corrode standard stainless steel hardware, causing spring failure and metallic gland pitting.
Elastomer Chemical Swelling
Standard O-rings swell, crack, or dissolve in volatile solvents, causing secondary seal blowouts.
Fugitive Toxic Emissions
Strict environmental standards mandate zero leakage of hazardous chemical vapors into plant atmosphere.
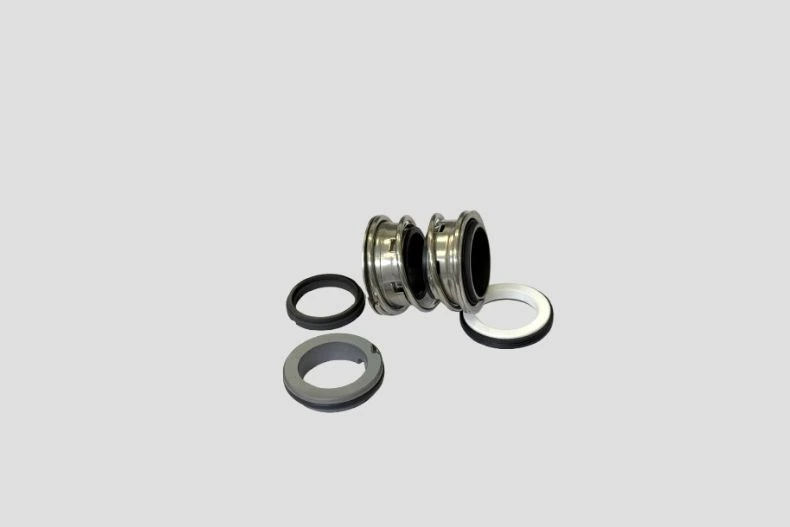
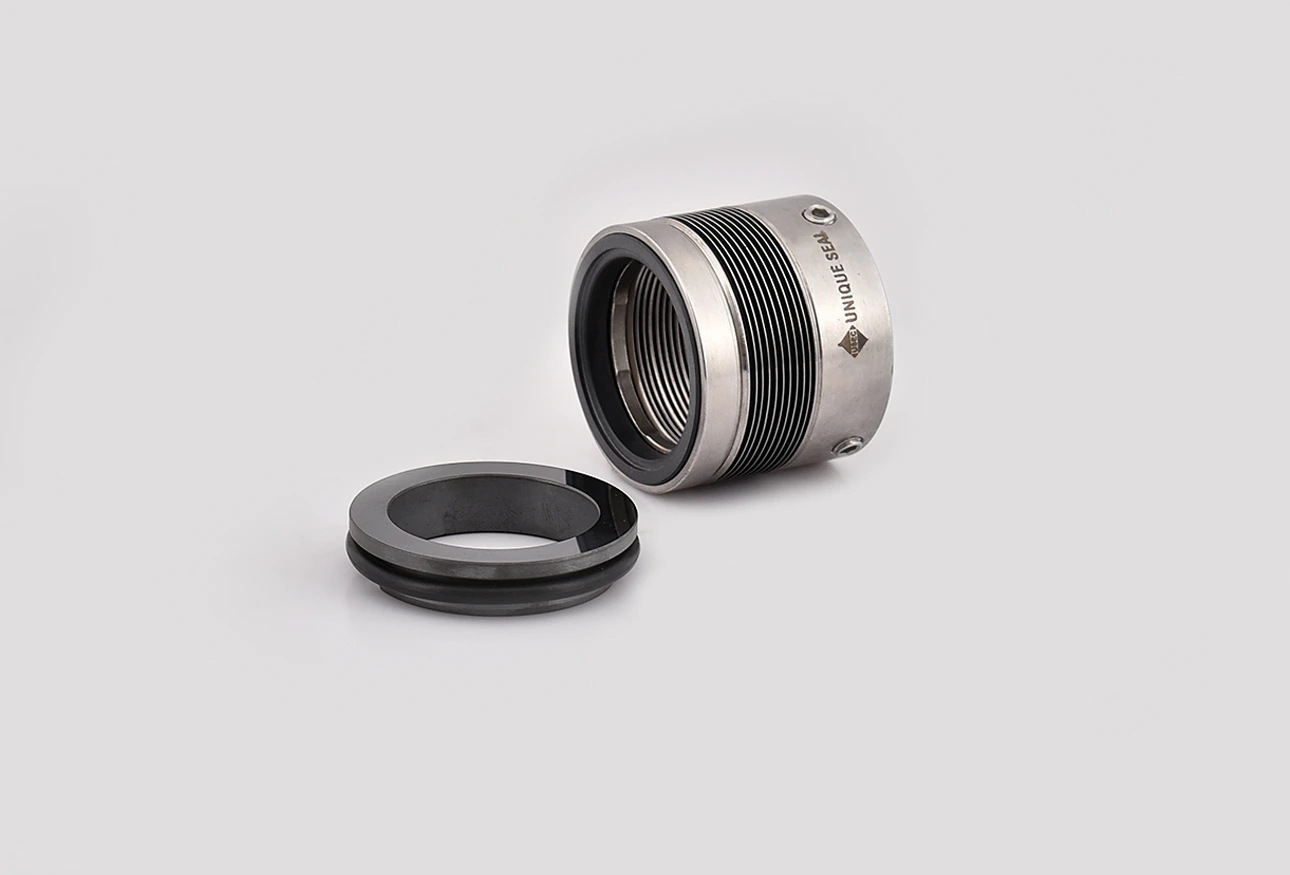
Recommended Mechanical Seals for Chemical Processing
Specialty Chemical Manufacturer in Dahej Industrial Estate, Gujarat
Verified Plant Outcome
The Problem
Frequent seal failure on 70% hot nitric acid and solvent extraction pumps. The existing OEM mechanical seals failed within 18-24 days due to elastomer degradation and metallic spring corrosion, creating acute OSHA safety hazards.
USEC Solution
USEC engineered and supplied US-TB PTFE composite bellows mechanical seals fitted with monolithic reaction-bonded silicon carbide seal faces and Hastelloy-C clamping rings, eliminating all vulnerable metallic components.
Quantified Result
Mean Time Between Failures (MTBF) increased from 3 weeks to over 18 continuous months. Hazardous chemical leakage was completely halted, saving an estimated ₹14.5 Lakhs annually in maintenance and product loss.
Quality Standards
Why Industry Leaders Choose USEC Mechanical Seals
100% Optical Flat Tested
Helium monochromatic light verification for sub-micron face flatness.
Certified Metallurgy
Full 3.1 MTC certificates for SS316, Hastelloy-C, Silicon Carbide & FFKM.
24-48 Hr Fast Dispatch
Rapid supply across India and global exports to eliminate pump downtime.
Technical Consultation
Need a Custom Sealing Solution for Your Chemical Processing Pumps?
Our application engineers visit plants, inspect failed seals, and design custom dimension mechanical seals with guaranteed leak-free performance.