Need Help: All Types of Mechanical Seals & Spares, Call 0120-4923910
Distillation Sealing Solutions
OEM Engineered Industry Solutions
Distillation Mechanical Seals & Sealing Systems
Engineering Focus: Explosion-Proof & Leak-Free Sealing for Ethanol Distillation, Solvent Recovery, and Mash Pumps
Distilleries, ethanol plants, and solvent recovery units operate in hazardous flammable environments where zero vapor emissions are paramount. Transferring fermented wash, spent wash, concentrated ethanol, and volatile aldehydes demands mechanical seals that withstand both abrasive spent grains and explosive alcohol vapors. USEC designs ATEX-compliant dual seals and cartridge systems.
Distillation processes require high precision and hygiene. Our seals ensure trouble-free pumping, mixing, and fermentation. Seal operations in pumps, mixers, and fermentation tanks will be leak-proof and clean.
We support distilleries in achieving operational efficiency while ensuring the highest quality standards are met by designing our solutions for high performance and durability.
Critical Operating Challenges in Distillation
Flammable Ethanol Vapor Leakage
Volatile spirit vapors escaping pump stuffing boxes create dangerous fire and explosion risks in distillation columns.
Abrasive Spent Wash Slurry
Fermented grain mash and spent wash contain coarse abrasive solids that score standard pump seal faces.
High Temperature Boiling Cycles
Continuous reflux temperatures near 100°C flash volatile fluids into vapor across the seal interface.
120 KLPD Grain-Based Biofuel Distillery in Bareilly, Uttar Pradesh
Verified Plant Outcome
The Problem
Primary fermented wash transfer pumps experienced seal face blowout every 15 days due to grain grit erosion and flashing of alcohol vapors across the unpressurized seal face.
USEC Solution
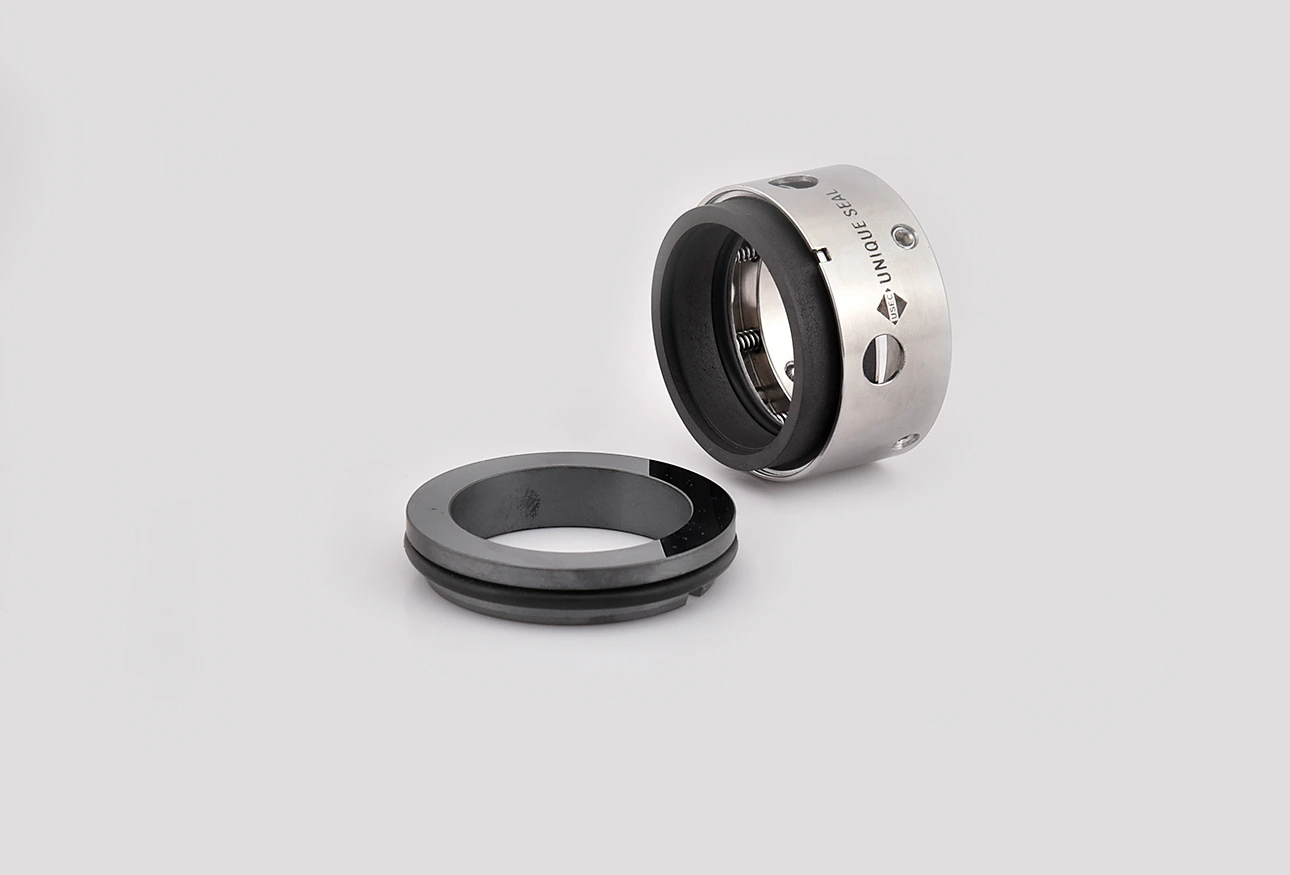
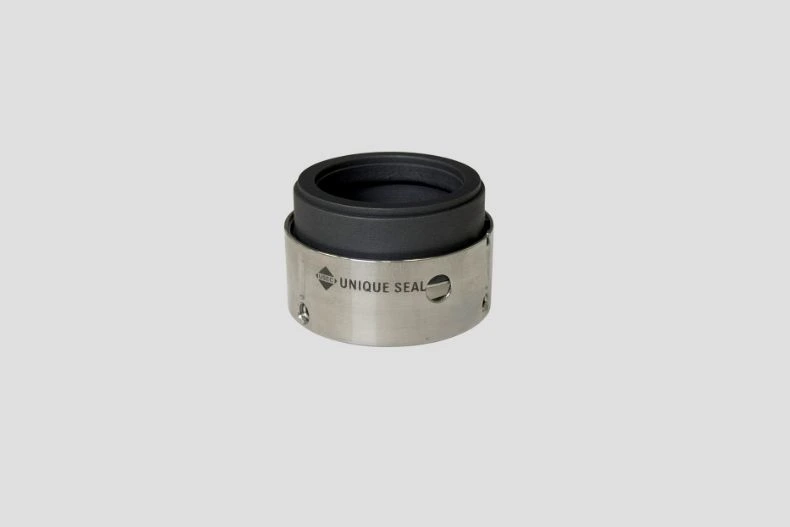
USEC engineered and installed US 043 DBL double wave spring mechanical seals with API Plan 53A thermosiphon barrier fluid circulation, preventing atmospheric vapor release.
Quantified Result
Achieved 100% leak-free containment with zero ethanol aroma around pump pads and increased continuous seal longevity to over 15 months.
Quality Standards
Why Industry Leaders Choose USEC Mechanical Seals
100% Optical Flat Tested
Helium monochromatic light verification for sub-micron face flatness.
Certified Metallurgy
Full 3.1 MTC certificates for SS316, Hastelloy-C, Silicon Carbide & FFKM.
24-48 Hr Fast Dispatch
Rapid supply across India and global exports to eliminate pump downtime.
Technical Consultation
Need a Custom Sealing Solution for Your Distillation Pumps?
Our application engineers visit plants, inspect failed seals, and design custom dimension mechanical seals with guaranteed leak-free performance.